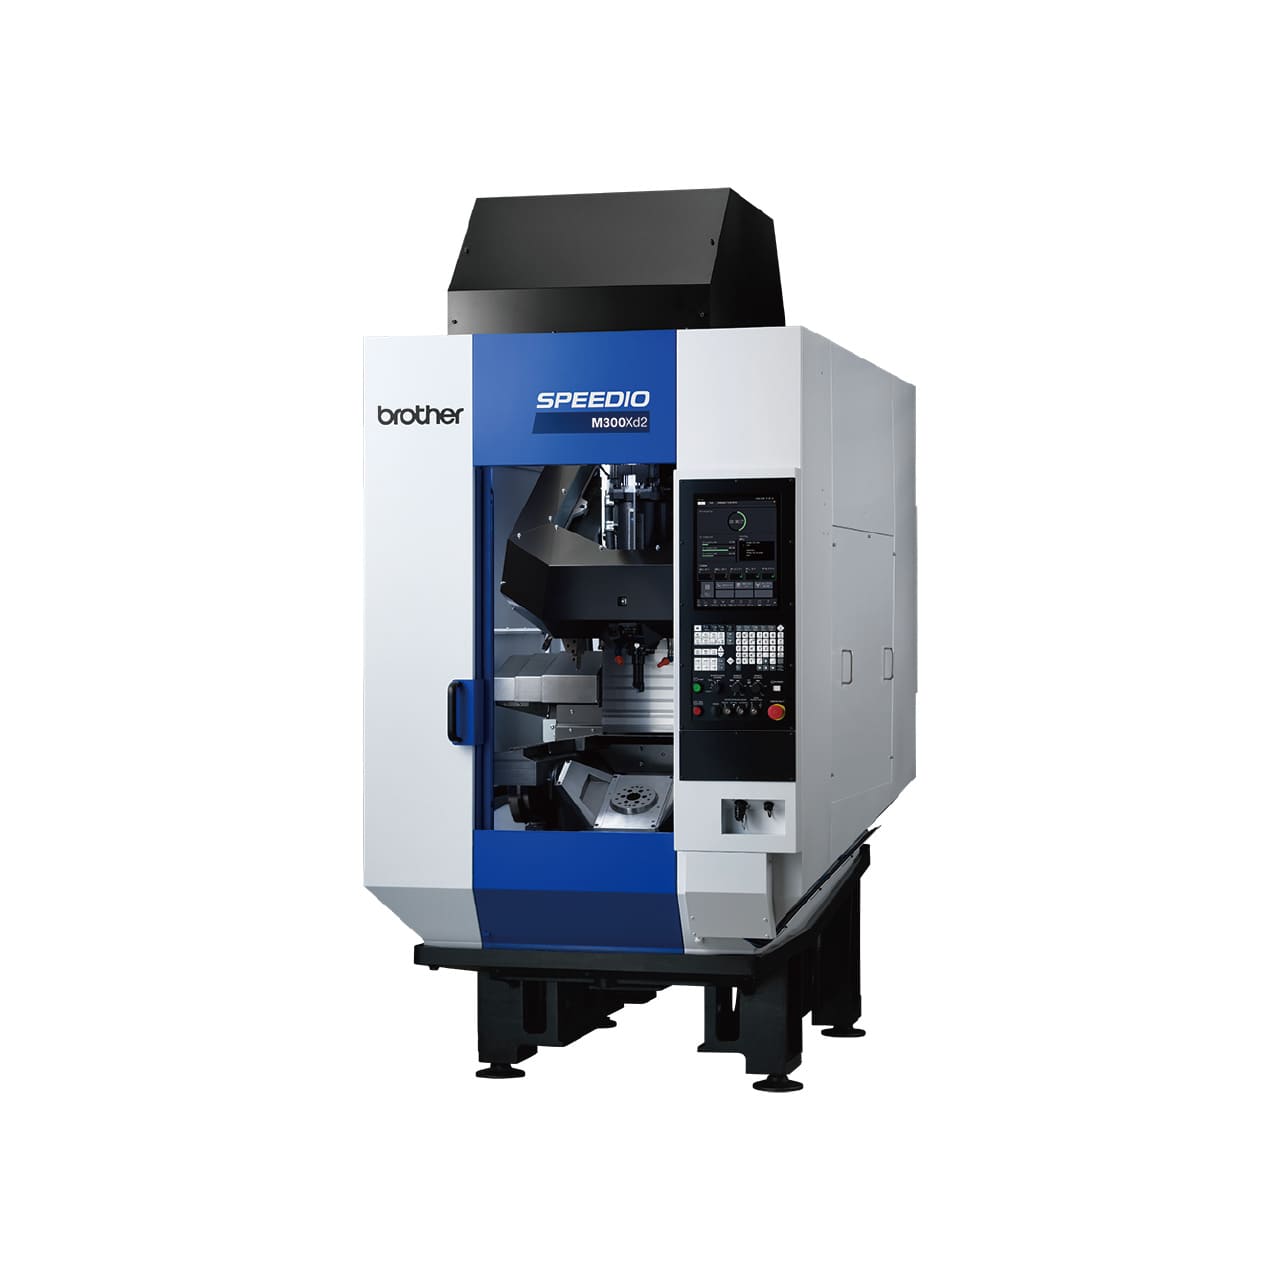
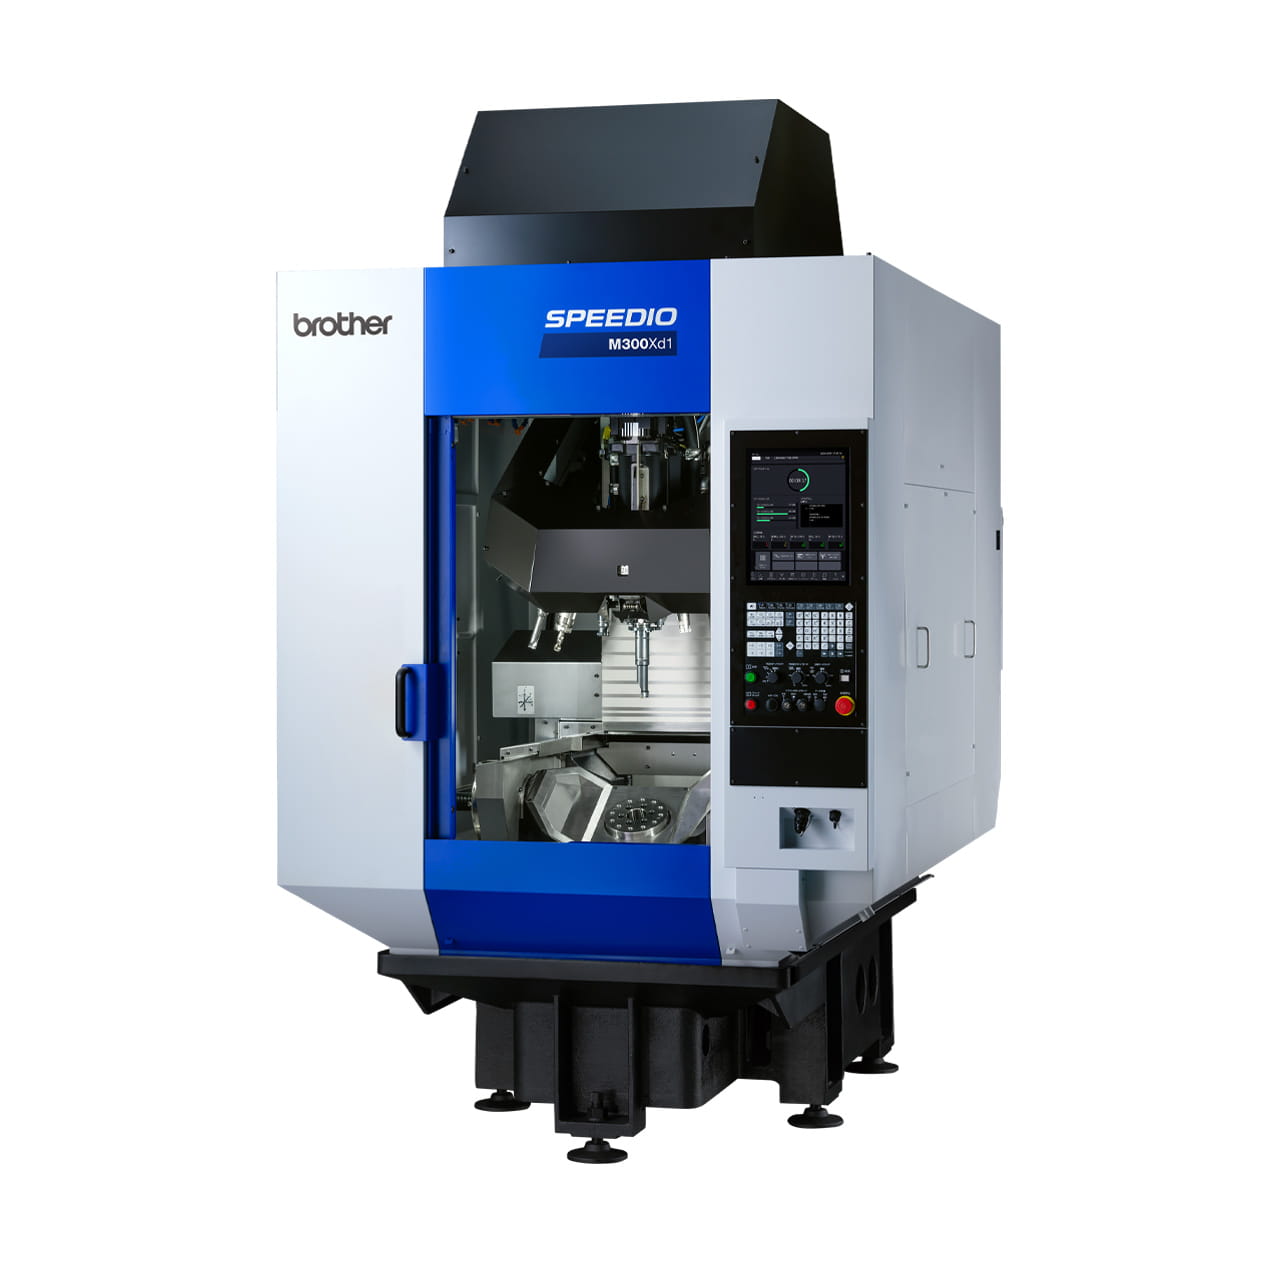
SPEEDIO M300Xd2
Compact Multi-Tasking Machine
- Travels [mm (inch)]: X: 300(11.8) Y: 440(17.3) Z: 380(15.0)
- Travels (A, C) (deg.): A: -30 to 120, C: 360
- Max. spindle speed (min-1): 12,000/ (Optional) 10,000 high-torque/ (Optional) 20,000/ (Optional) 27,000
- Tool storage capacity(pcs.): 21/ 28
- Max. turning spindle speed (min-1): C-axis standard: 2,000/ C-axis high-torque: 1,500
Select variant: M300Xd2
[ BT30 Vertical multi-tasking machine ]
Multi-tasking machine capable of
turning and milling in a single setup
Enables process integration with a smaller footprint
Information


Overview
Benefits of process integration with mass production type multi-tasking machine
[1] Reduction of handling time between machines
[2] Easier process balancing
[3] Improvement of machining accuracy through one-time chucking
Equipped with a tilting rotary table with turning functions, the machine enables integration of a wide range of machining processes, from multi-tasking to multi-face machining, offering various benefits such as reduced handling time.
High-productivity, mass-production multi-tasking machining enhances the efficiency of mass production lines.
Reduction of handling time
Turning and milling can be completed through one-time chucking on one machine.
This model eliminates handling between the lathe and the machining center, thus reducing the number of operators needed. One-time chucking also improves machining accuracy.

Improvement of process balance
Integration of turning and milling processes into one machine improves process balance, leading to increased productivity.
Additionally, in the event of a problem, production can continue easily as all processes are completed on one machine.


Ample machining area tailored to C-axis specifications
Two jig areas are provided to accommodate C-axis specifications. For the high-torque C-axis specification, a jig area of up to ⌀ 450 mm can be secured by restricting certain movements. Furthermore, the 380 mm Z-axis travel and 100 mm spindle lowest point ensure ample machining area in the Z-axis direction and excellent tool accessibility.
*1. Value when A-axis is at 0°.
*2. The jig area has some interference areas depending on the movement of each axis and the tool size. For details, please refer to the external views or interference diagrams provided by Brother.
*3. Max. loading capacity on table side
*4. Values for low table specification.

Tool accessibility when tilting the A-axis
The 380 mm Z-axis travel provides excellent tool accessibility, while ensuring sufficient Y-axis travel even when the A-axis is at 90°.

Low-table specification and maximum tool length
The C-axis high-torque specification offers a low-table option. Combined with a maximum tool length of 250 mm, it is capable of machining tall workpieces such as motor cases.
Low table specification
Distance between table top and spindle nose end
150 to 530mm
Maximum tool length
250mm
* Tools with a length of 200 mm or more may contact the jig when the magazine turns, depending on the jig height.


Milling
A high-torque specification (optional) with a maximum torque of 92 N・m has been added, delivering superior machining performance for tasks such as large-diameter hole machining. Various spindle specifications are available, including the standard 12,000 min-1 and the optional 20,000 min-1 specifications.
High-torque spec.(optional)
Max. torque 92N・m
Max. output 26.2kW
20,000min-1 spec.(optional)
Max. torque 27N・m
Max. output 15.4kW
12,000min-1 spec.(standard)
Max. torque 40N・m
Max. output 18.9kW

Turning
A standard specification with a maximum speed of 2,000 min-1 and an optional high-torque specification with a maximum torque of 102 N・m are available. Turning tools secured by a double plunger lock mechanism enable efficient machining.
Turning spindle (C-axis)
C-axis standard: Turning spindle speed 2,000min-1, Max. torque 55N・m, Max. output 8.7kW
C-axis high-torque: Turning spindle speed 1,500min-1, Max. torque 102N・m, Max. output 9.9kW

Vibration adjustment (optional)
Vibration adjustment is a function that analyzes waveform data using a PC app and suggests recommended spindle speeds. By suggesting optimal machining conditions, it is able to maximize machining performance.

A-axis clamp (optional)
The mechanical clamp plus servo clamp method enables the machine to demonstrate high machining capabilities in high-load machining and stable lathe turning, improving machining accuracy. A double type clamp mechanism, where clamps are provided on the left and right sides, is available to further enhance high machining capabilities.
A-axis clamp torque *2
C-axis standard: Single 695N・m Double 975N・m
C-axis high-torque: Single 800N・m Double 1,080N・m
*1. Only driving side for single type
*2. Value of mechanical clamp (at pneumatic 0.5 MPa) plus servo clamp
A-axis clamp (double) *1

High-speed spindle spec. (optional) compatible with CTS
A 27,000 min-1 specification (optional) compatible with coolant through spindle (CTS) is also available. Combined with functions such as look-ahead and smooth path offset function, it enables high-speed and highly accurate three-dimensional machining.
High-speed spindle spec. (optional) 27,000min-1
High accuracy mode BII (optional) Look-ahead 1,000 blocks
C-axis clamp
The C-axis with high clamp force enables more stringent cutting conditions to be set for machining that results in load being applied in the rotational direction, improving production efficiency.
C-axis clamp torque
C-axis standard 345N・m
C-axis high-torque 450N・m
Simultaneous 5-axis machining *
Equipped with various functions such as tool center point control and submicron command, combined with a backlash-free tilting rotary table, this machine achieves high-speed and highly accurate simultaneous 5-axis machining.
*Available only on the M300Xd2-5AX.
Tool center point control
Equipped with tool center point control where machining is performed by changing the tool direction relative to the workpiece. Optimal acceleration by look-ahead up to 1,000 blocks and two types of control (G43.4 and G43.5) achieve simultaneous 5-axis machining.

Processing speed of minute line segments
The CPU capacity has been greatly increased to enhance the processing speed of minute line segments by four times the previous controller. This enables high-speed processing of CAM data with small tolerance.

Spindle/turning spindle synchronized control (optional)
Synchronized rotation of the spindle and turning spindle at the instructed rotation ratio enables gear cutting, such as hobbing and skiving.
In addition, the phase angle compensation function of the turning spindle relative to the spindle enables helical gear cutting.


Non-stop ATC
High-speed tool change has been achieved by faster and optimized spindle start/stop and magazine operation.
21-tool magazine
Chip to Chip 1.3s
Tool to Tool 0.6s
High acceleration/deceleration spindle
The low inertia spindle and high acceleration/deceleration spindle motor ensure faster spindle start/stop. In addition, the turning spindle with DD motor achieves high acceleration/deceleration speed.
Spindle start/stop time
Machining spindle 0.2s or less
Turning spindle 0.3s or less
Simultaneous operation
Wasted time has been reduced by simultaneously performing tool change and positioning X/Y and A/C axes.

High-speed indexing
High-speed indexing has been achieved for both the clampless (standard) tilt axis (A-axis) and the turning spindle with indexing function. For the tilt axis, the clamp mechanism can be optionally selected.
Indexing feed rate
C-axis standard: A-axis 60min-1, C-axis 200min-1
C-axis high-torque: A-axis 50min-1, C-axis 200min-1
0 to 90° Indexing time
C-axis standard: A-axis 0.6s, C-axis 0.7s
C-axis high-torque: A-axis 0.7s, C-axis 0.7s
Optimized A/C-axes indexing feed rate
Based on the estimated A/C-axes inertia, the A/C-axes start with optimal acceleration until they reach the indexing feed rate.

Machining support without warmup
Equipped with an original measurement processing function that reduces the number of actual measurements by a touch probe according to the size of displacement. This eliminates the need for warmup operation, minimizing effects on productivity and ensuring high-accuracy machining.

Base shape with excellent chip evacuation
In addition to the conventional center trough structure, the base shape has been redesigned to prevent chips from accumulating. The base is sloped from back to front, and the chip shower piping has been optimized, resulting in a significant improvement in chip evacuation compared to previous models.

Oscillating cutting function (optional)
This function vibrates the axis in the cutting direction and synchronously controls this vibration with the rotation of the turning spindle. By creating air cuts during machining, it enables intermittent cutting and breaks up chips.

Reliability features to prevent troubles
The machine is equipped with many functions that can prevent possible defects in daily production sites, such as chip problems, tool abrasion, omission of tool attachment, and re-machining of the same workpiece. These functions help reduce wasted resources at production sites.
・Stuck chips detection function
・Tool cleaning system
・ATC tool monitoring
・Machining load monitoring (spindle/turning spindle)

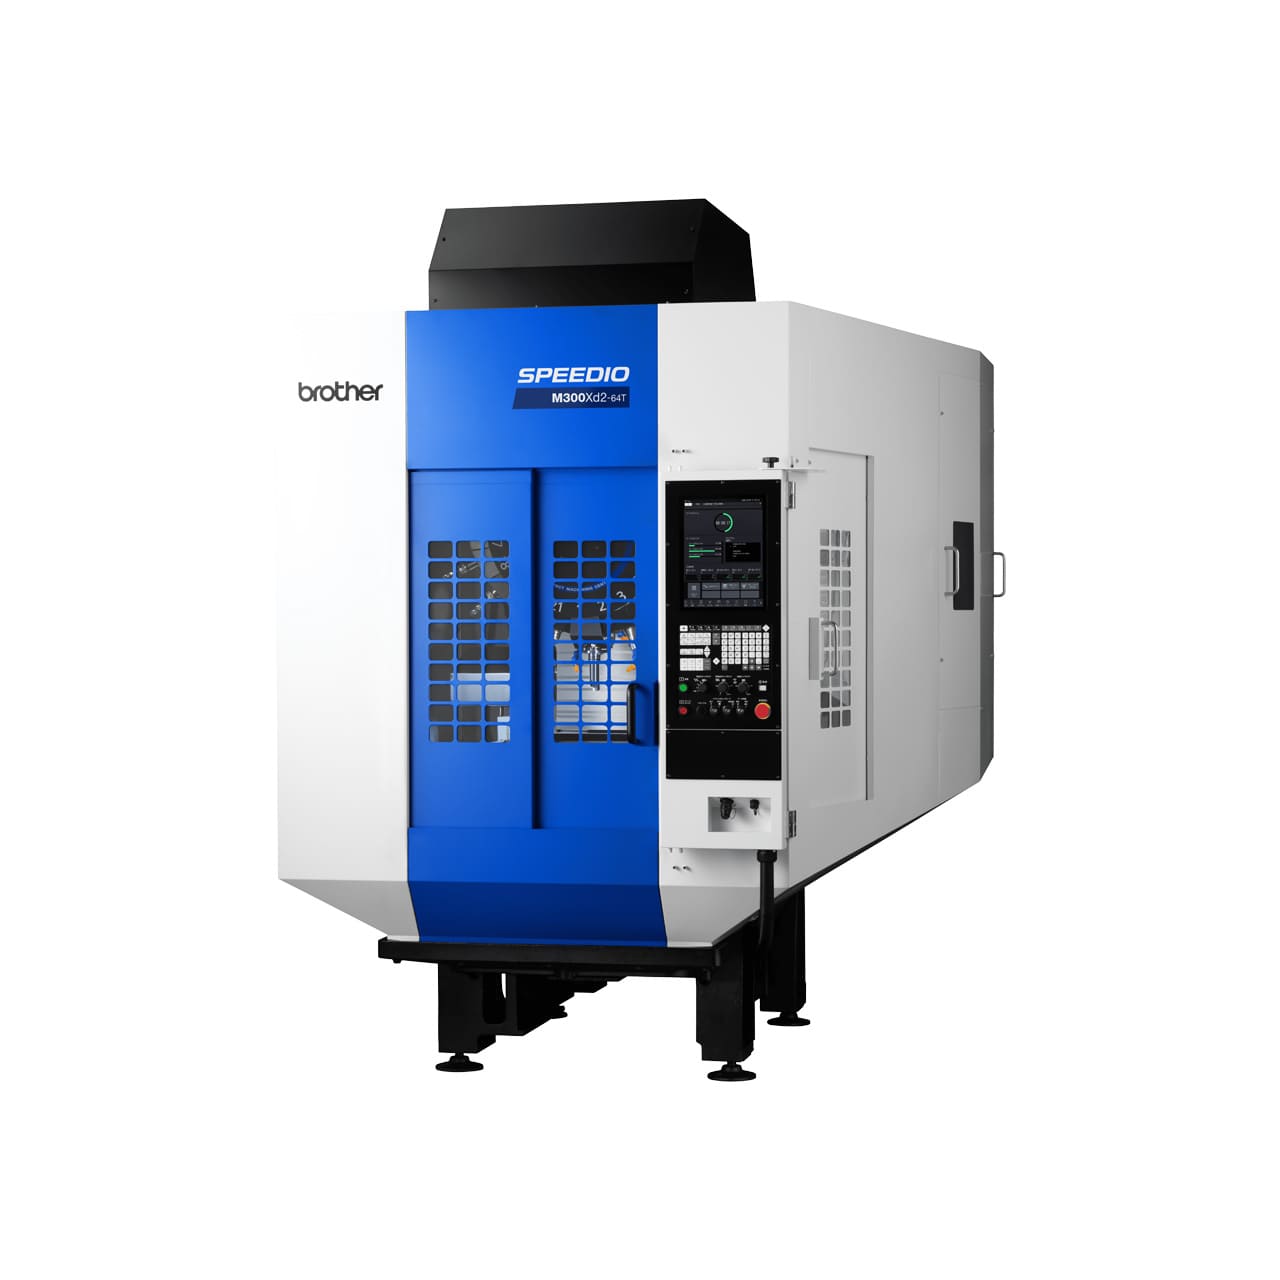
Capable of handling small-lot, multi-variety production with a 64-tool magazine and a tilting rotary table with turning functions
Equipped with a newly developed 64-tool magazine and a tilting rotary table with turning functions, this machine can handle high-mix small-lot production including turning process.
Integration of milling and turning processes reduces equipment investment, saving manpower.

Newly developed 64-tool magazine
In addition to the 21-tool turret magazine, a tool stocker that holds 43 tools has been added on the right side, allowing storage of up to 64 tools.
Brother’s original tool handling mechanism ensures stable tool change.
64-tool magazine specification
Turret magazine: 21tools
Tool stocker: 43tools
Total: 64tools
High reliability
The stocker shutter separates the tool stocker from the machining chamber, minimizing the effect of chips on tools.

Space saving
Tool stockers, which can store 64 tools, are installed inside the machine to save space.
*1. Does not include coolant tank and chip conveyor.
*2. Compared to BT40 vertical MC with equivalent tool storage capacity.

High productivity
If the number of tools used in machining is 21 or less, high speed tool change is possible using only the turret magazine, leading to high productivity. Even when using tools in the tool stocker, handling is possible within approximately 5 seconds (1 tool).
In addition, all tools in the turret magazine can be easily changed, reducing setup time.
Turret magazine tool change time
Tool to Tool: 0.6S
Chip to Chip: 1.3S
Tool stocker handling time*3
Shortest (1 tool) Approx. 6S*4
All tool change (21 tools) Approx. 90S
*3.Handling time varies depending on the tool attachment position.
*4.Time for the tool at the spindle position to be moved and changed with a tool in the tool stocker and for this tool to return to the spindle position.
Specifications
Product Specification
M300Xd2
Max. spindle speed [min⁻¹]
12,000/ (Optional) 10,000 high-torque/ (Optional) 20,000/ (Optional) 27,000
Travels [mm (inch)]
X: 300(11.8) Y: 440(17.3) Z: 380(15.0) A(deg.):-30 to 120 C(deg.):360
Tool storage capacity [pcs.]
21 / 28
Rapid traverse rate (XYZ axes) [m/min (inch/min)]
50 x 50 x 50 (1,969 x 1,969 x 1,969)
Indexing feed rate [min⁻¹]
C-axis standard: A: 60 C: 200/ C-axis high-torque: A: 50 C: 200
Required floor space [mm (inch)]
21 tools:1,590 x 2,697 (62.6 x 106.2) 28 tools:1,300 x 2,667 (51.2 x 105.0)
BT dual contact spindle(BIG-PLUS)
Optional
Coolant Through Spindle(CTS)
Optional
| Item | M300Xd2 M300Xd2 RD*8 M300Xd2-5AX M300Xd2-5AX RD*8 |
M300Xd2-64T M300Xd2-64T RD*8 M300Xd2-5AX/64T M300Xd2-5AX/64T RD*8 |
||
|---|---|---|---|---|
| CNC Unit | 《M300Xd2》CNC-D00 《M300Xd2-5AX》CNC-D00v (DB) | |||
| Travels | X axis [mm(inch)] | 300 (11.8) | ||
| Y axis [mm(inch)] | 440 (17.3) | |||
| Z axis [mm(inch)] | 380 (15.0) | |||
| A axis [deg.] | -30 - 120 | |||
| C axis [deg.] | 360 | |||
| Distance between table top and spindle nose end [mm(inch)] | C-axis standard spec.: 100 - 480 (3.9 - 18.9)*15 C-axis high-torque spec.: 100 - 480 (3.9 - 18.9)*15 [Low table spec.: 150 - 530 (5.9 - 20.9)]*15 |
|||
| Table | Work area size [mm(inch)] | C-axis standard spec.: ⌀140 (⌀5.5) C-axis high-torque spec.: ⌀170 (⌀6.7) |
||
| Shape of table top | C-axis standard spec.: In compliance with table nose No.5 of ISO702-4 (JISB6109-2) C-axis high-torque spec.: In compliance with table nose No.6 of ISO702-4 (JISB6109-2) |
|||
| Max. loading capacity (uniform load) [kg(lbs)] |
C-axis standard spec.: Table side 40 (88) / Tale side 19 (42)*9 C-axis high-torque spec.: Table side 75 (165) / Tale side 19 (42)*9 |
|||
| Max. table load inertia [kg・m2(lb・inch2)] |
C-axis standard spec.: Table side 0.29 (991) / Tale side 0.04 (137) C-axis high-torque spec.: Table side 0.8 (2,734) / Tale side 0.04 (137) |
|||
| Spindle | Spindle speed [min-1] | 12,000min-1 spec.: 1 - 12,000 10,000min-1 high-torque spec.(Optional): 1 - 10,000 20,000min-1 spec.: (Optional): 1 - 20,000 27,000min-1 spec.(Optional)*13: 1 - 27,000 |
||
| Speed during tapping [min-1] | MAX. 6,000 (27,000min-1 spec.: MAX 8,000) | |||
| Tapered hole | 7/24 tapered No.30 | |||
| BT dual contact spindle (BIG-PLUS) | Optional | |||
| Coolant Through Spindle (CTS) | Optional | |||
| Turning spindle | Max. spindle speed [min-1] | 2,000/1,500 (C-axis standard spec. / C-axis high-torque spec.) | ||
| Feed rate | Rapid traverse rate (XYZ-area) [m/min(inch/min)] |
50 x 50 x 50 (1,969 x 1,969 x 1,969) | ||
| Cutting feed rate [mm/min(inch/min)] |
X, Y, Z axes: 1 - 30,000 (0.04 - 1,181)*7 | |||
| Indexing feed rate (A and C) [min-1] |
A-axis: 60/50(C-axis standard spec. / C-axis high-torque spec.) C-axis: 200 | |||
| ATC unit | Tool shank type | MAS-BT30 | ||
| Pull stud type*4 | MAS-P30T-2 | |||
| Tool storage capacity [pcs.] | 21/28*10 | 64*14 | ||
| Max. tool length [mm(inch)]*1 | 250 (9.8)*12 | 250 (9.8)*12 | ||
| Max. tool diameter [mm(inch)]*1 | 80 (3.1) | Turret magazine: 80(3.1), Tool stocker: 60 (2.3) / 80 (3.1) (No adjacent tool) |
||
| Max. tool weight [kg(lbs)]*1 | 3 (6.6) [total tool weight: 35 (77.2) for 21 tools, 40 (88.2)for 28 tools] | Turret magazine: 3 (6.6) [Total tool weight: 35 (77.2)] Tool stocker: 3 (6.6) [Total tool weight: 60 (132.3)] |
||
| Tool selection method | Random shortcut method | |||
| Tool change time*5 | Tool To Tool [sec.] | 0.6/0.8 (21 tools/28 tools) | 0.6*16 | |
| Chip To Chip [sec.] | 1.3/1.4 (21 tools/28 tools) | 1.3*16 | ||
| Electric motor | Main spindle motor (10 min/continuous) [kW]*2 | 12,000min-1 spec.: 10.1/7.0 10,000min-1high-torque spec. (Optional): 12.8/9.2 20,000min-1 spec. (Optional): 7.4/5.1 27,000min-1 spec. (Optional): 8.9/6.3 |
||
| Axis feed motor [kW] | X, Y axes: 1.0 Z-axis: 1.8 A-axis: 0.8/1.35 (C-axis standard spec./C-axis high-torque spec.) |
|||
| Turning spindle motor [kW] | 4.2/4.6 (C-axis standard spec./C-axis high-torque spec.) | |||
| Power source | Power supply | 200 to 230 VAC ±10%, 3phase, 50/60Hz±2% | ||
| Power capacity (continuous) [kVA] | 10.4 | |||
| Air supply | Regular air pressure [MPa] | 0.4 - 0.6 (recommended value 0.5MPa)*6 | ||
| Required flow [L/min] | 165 (27,000min-1 spec.: 175) | |||
| Machine dimensions | Height [mm(inch)] | 2,734 (107.6) | 2,734 (107.6) | |
| Required floor space*11 [mm(inch)] | 21 tools: 1,590 x 2,697 (62.6 x 106.2) 28 tools: 1,300 x 2,667 (51.2 x 105.0) |
1,935 x 2,731 (76.2 x 107.5) | ||
| Weight [kg(lbs)] | 2,750 (6,063) | 2,950 (6,504) | ||
| Accuracy*3 | Accuracy of bidirectional axis positioning (ISO230-2: 1988) | X, Y, Z axes: 0.006 - 0.020mm (0.00024 - 0.00079inch) | ||
| Repeatability of bidirectional axis positioning (ISO230-2: 2014) | X, Y, Z axes: Less than 0.004mm (0.00016inch) | |||
| Standard accessories | Instruction Manual (DVD 1 set), leveling bolts (4 pcs.), leveling plates(4 pcs.) | |||
- *1The maximum tool length, maximum diameter, and maximum weight are limited depending on the spindle speed in use, configuration, center of gravity, etc. The figures shown here are for reference only. Please contact your local distributor for details.
- *2Spindle motor output differs depending on the spindle speed.
- *3Measured in compliance with ISO standards and Brother standards. Please contact your local distributor for details.
- *4Brother specifications apply to the pull studs for CTS.
- *5Measured in compliance with JIS B6336-9 and MAS011-1987.
- *6Regular air pressure varies depending on the machine specifications, machining program details, or use of peripheral equipment. Set the pressure higher than the recommended value.
- *7Value when using high accuracy mode B and tool center point control.
- *8The machine needs to be equipped with a relocation detection device depending on the destination. Machines equipped with a relocation detection device have “RD” at the end of the model name.
- *9The loading capacity on the tail side is 13 kg at the rotating section and 6 kg at the fixed section.
- *10For the 28-tool magazine, turning tools cannot be set in adjacent pods.
- *11Dimensions not including the coolant tank and chip conveyor.
- *12Tools with a length of 200 mm or more may contact the jig when the magazine turns, depending on the jig height.
- *13For CTS specifications, a BT dual-contact spindle is used.
- *14Value for turret magazine plus tool stocker.
- *15The values differ when the pallet clamp is selected. Refer to the interference drawings provided by Brother for details.
- *16Value for turret magazine.
| Item | M300Xd2 | M300Xd2-5AX | |
|---|---|---|---|
| CNC model | CNC-D00 | CNC-D00v (DB) | |
| Control axes | 5 axes (X, Y, Z, A, C) | ||
| Simultaneously controlled axes | Positioning | 5 axes (X, Y, Z, A, C) | |
| Interpolation | Linear: 4 axes (X, Y, Z, 1 additional axis) Circular: 2 axes Helical/Conical: 3 axes (X, Y, Z) |
Linear: 5 axes (X, Y, Z, 2 additional axes) Circular: 2 axes Helical/Conical: 4 axes (3 linear axes + 1 additional axis, 2 linear axes + 2 additional axes) |
|
| Least input increment | 0.001 mm, 0.0001 inch, 0.001° 0.0001 mm, 0.00001 inch, 0.0001° (optional) |
0.0001 mm, 0.00001 inch, 0.0001° | |
| Max.programmable dimension | ±999999.999 mm, ±99999.9999 inch ±999999.9999 mm, ±99999.99999 inch (optional) |
±999999.9999 mm, ±99999.99999 inch | |
| Display | 15-inch color LCD touch display | ||
| Memory capacity | 500 Mbytes, 3 Gbytes (optional) (Total capacity of program and data bank) |
3 Gbytes (Total capacity of program and data bank) |
|
| External communication | USB memory interface, Ethernet, RS232C (optional) | ||
| No.of registrable programs | 4,000 (Total capacity of program and data bank) | ||
| Program format | NC language * Conversation language not available | ||
- *“Control axes” and “Simultaneously controlled axes” indicate the maximum number of axes, which will differ depending on the shipping destination or machine specifications.
- *Ethernet is a registered trademark of Xerox Corporation in the United States.
| Operation | Dry run Machine lock Program restart Rapid traverse override Cutting feed override Background editing Screen shot Operation level External input signal key Shortcut key < optional > |
|---|---|
| Programming | Absolute / incremental Inch / metric Coordinate system setting Corner C / Corner R Rotational transformation Synchronized tap Subprogram Graphic display |
| Measurement | Automatic workpiece measurement *1 Tool length measurement |
| High speed and high accuracy |
Machining parameter adjustment High accuracy mode AIII High accuracy mode BI (look-ahead 160 blocks) Backlash compensation Tool center point control *2 (Look-ahead 1,000 blocks) < optional > |
| Monitoring | Machining load monitoring ATC tool monitoring Overload prediction Waveform display / Waveform output to memory card Automatic thermal distortion compensation (X, Y, and Z axes) Production performance display Tool life / Spare tool Stuck chips detection function |
| Maintenance |
Tap return function Status log Alarm log Operation log Maintenance notice Motor insulation resistance measurement Tool cleaning filterwith filter clogging detection Battery-free encoder Brake load test |
| Automatic / Network | Computer remote OPC UA Auto notification Built-in PLC (LD/ST/FBD) < optional > |
| Energy saving | Automatic power off Standby mode Automatic coolant off Automatic work light off Chip shower off delay Chip shower Energy-saving operation Energy-saving mode |
| Support apps | Machining parameter adjustment ATC tool Tool life Waveform display Production performance Energy saving/Power consumption Recovery support Inspection PLC Machining support without warmup Software control panel Machining program creation support function |
| Accessories | File viewer Notebook Calculator Register shortcut Display off |
| NC language functions | Menu programming Local coordinate system Expanded workpiece coordinate system One-way positioning Inverse time feed Programmable data input Tool length compensation Cutter compensation Scaling Mirror image External sub program call Macro Tape operation / FTP load operation Multiple skip function < optional > |
| Turning functions | Constant peripheral speed control Feed per revolution control Tool position compensation (X, Y, Z) Nose R compensation Tread cutting function < optional > |
- *1For the measuring instrument, please select an optional touch probe or provide one yourself.
- *2Available only on the M300Xd2-5AX.
- *3Standard on the M300Xd2-5AX.
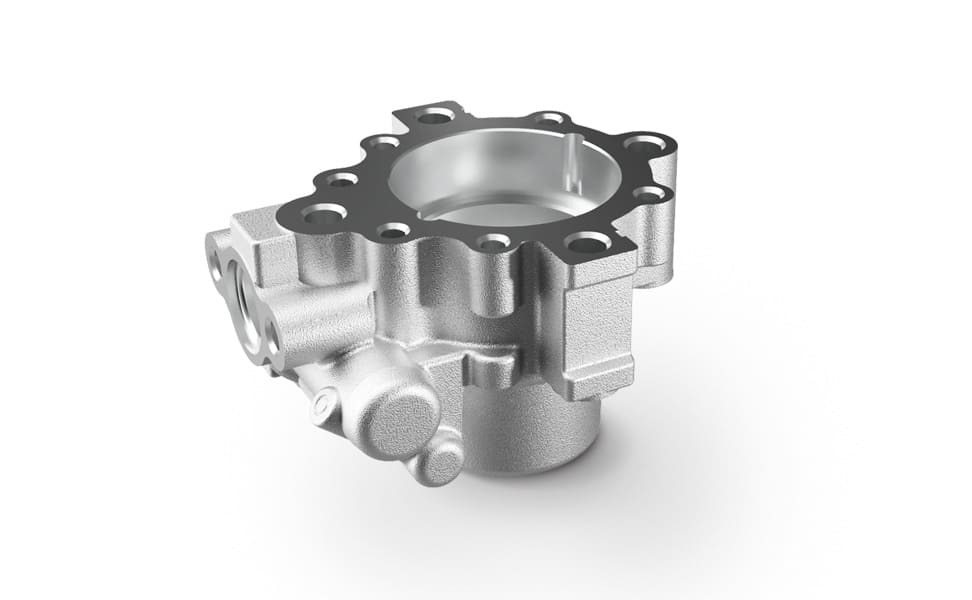
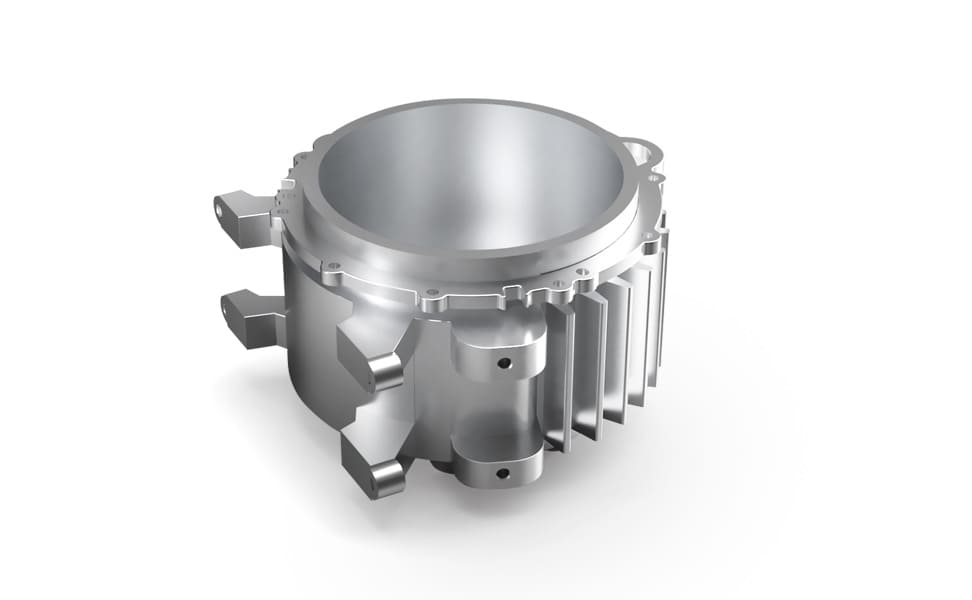
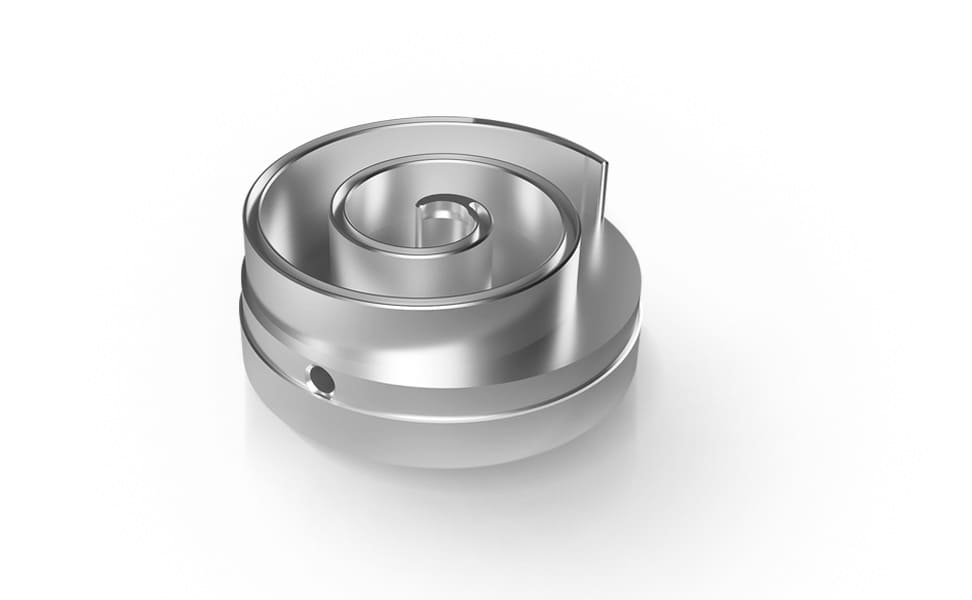
Example
Support
Support Information